Stamping. Welding. Sub-assembly. Tool & die.
Value-added, all in-house.
Clover Group is a Canadian custom metal stamping, metal forming, robotic welding and sub-assembly supplier — serving automotive, brake systems (disc and drum), heavy-duty truck, commercial-vehicle and industrial programs from Concord (GTA / Toronto) and Breslau (Waterloo region). Progressive, transfer and hand-transfer stamping, robotic welder cells and finished sub-assemblies, plus full in-house tool & die build. Every program from RFQ to SOP managed on one APQP workflow.
Metal Stamping & Forming
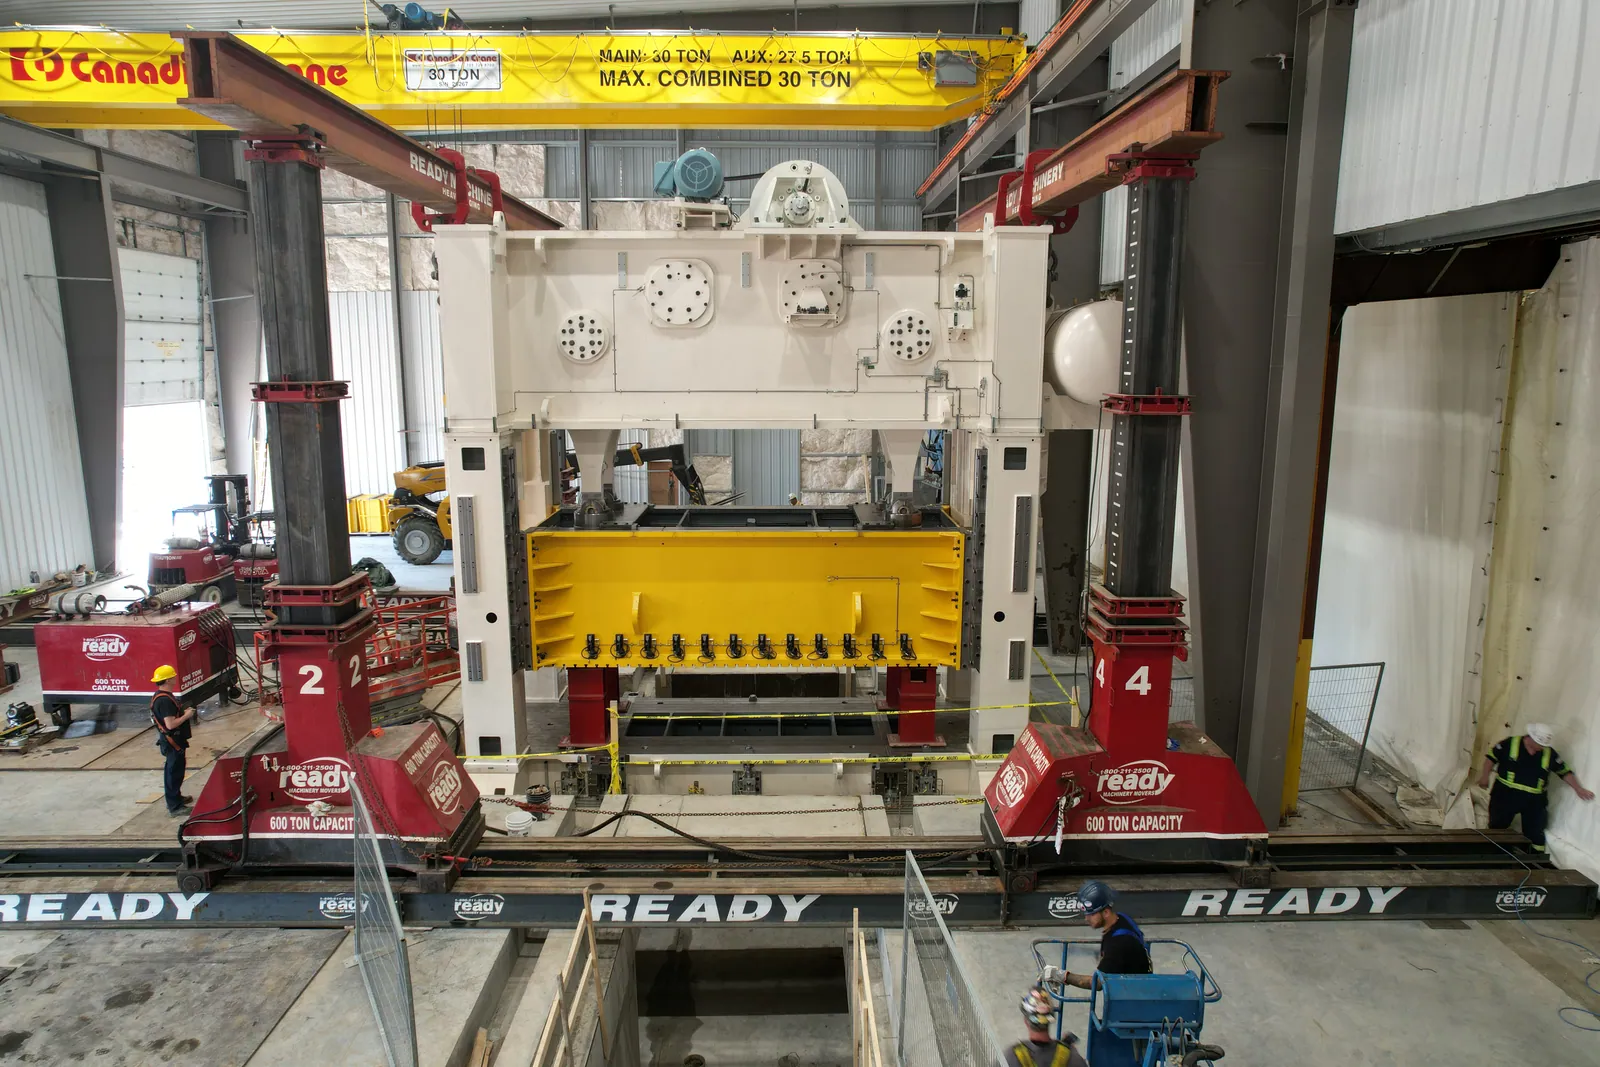
Progressive-die, mechanical-transfer and hand-transfer metal stamping and forming — 80 to 1,650 tons.
A 30-press fleet running customer programs from prototype to production. Small, high-volume parts on 80- to 300-ton presses; mid-volume transfer work on 500–800-ton presses; heavy stamping on the 1,650-ton line for chassis, body and commercial-vehicle components. In-die staking, tapping and nut welding eliminate downstream steps and keep piece price competitive. Custom metal stamping for automotive, heavy-duty truck, brake systems and industrial programs.
Welding
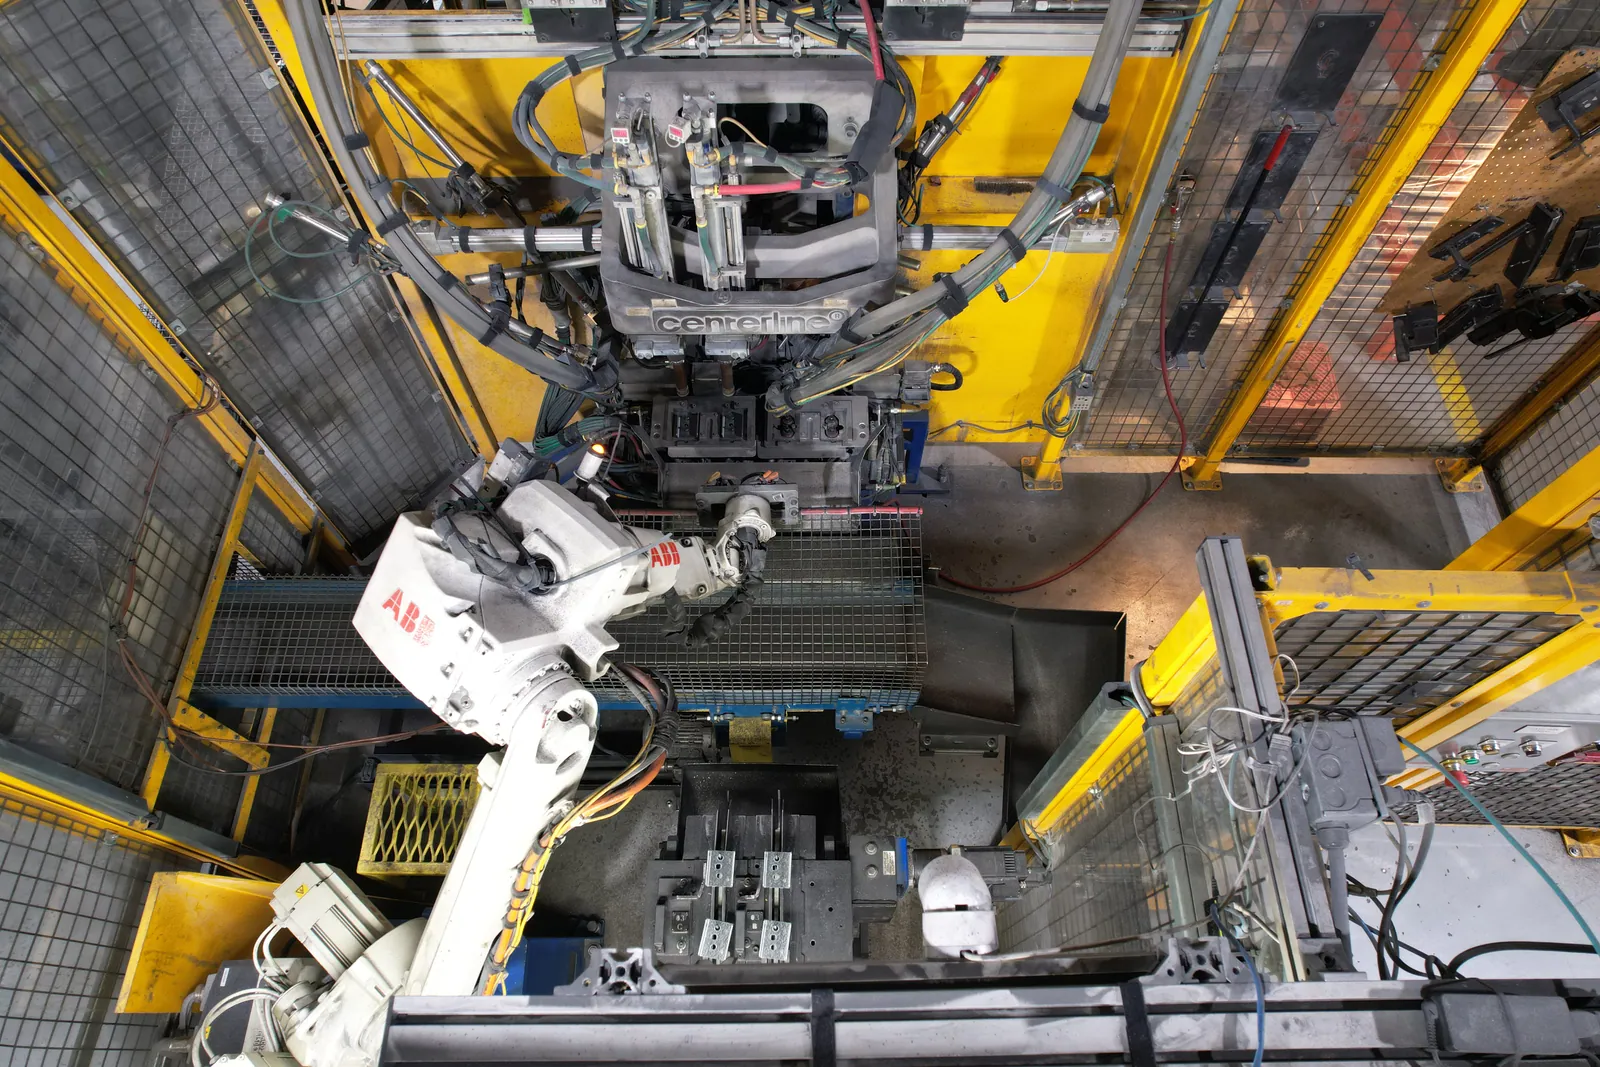
Robotic welders, projection, spot and specialty welding — cell-ready for high-mix programs.
Twelve robotic MIG welder cells run alongside 15+ projection welders and three spot welders. Specialty welding on a Flexfast nut-and-stud welder and a Norton bushing install cell. Every welded part is traceable to its coil. Robotic welding cells deployed across automotive, brake systems, commercial-vehicle and heavy-duty truck programs.
Sub-Assembly
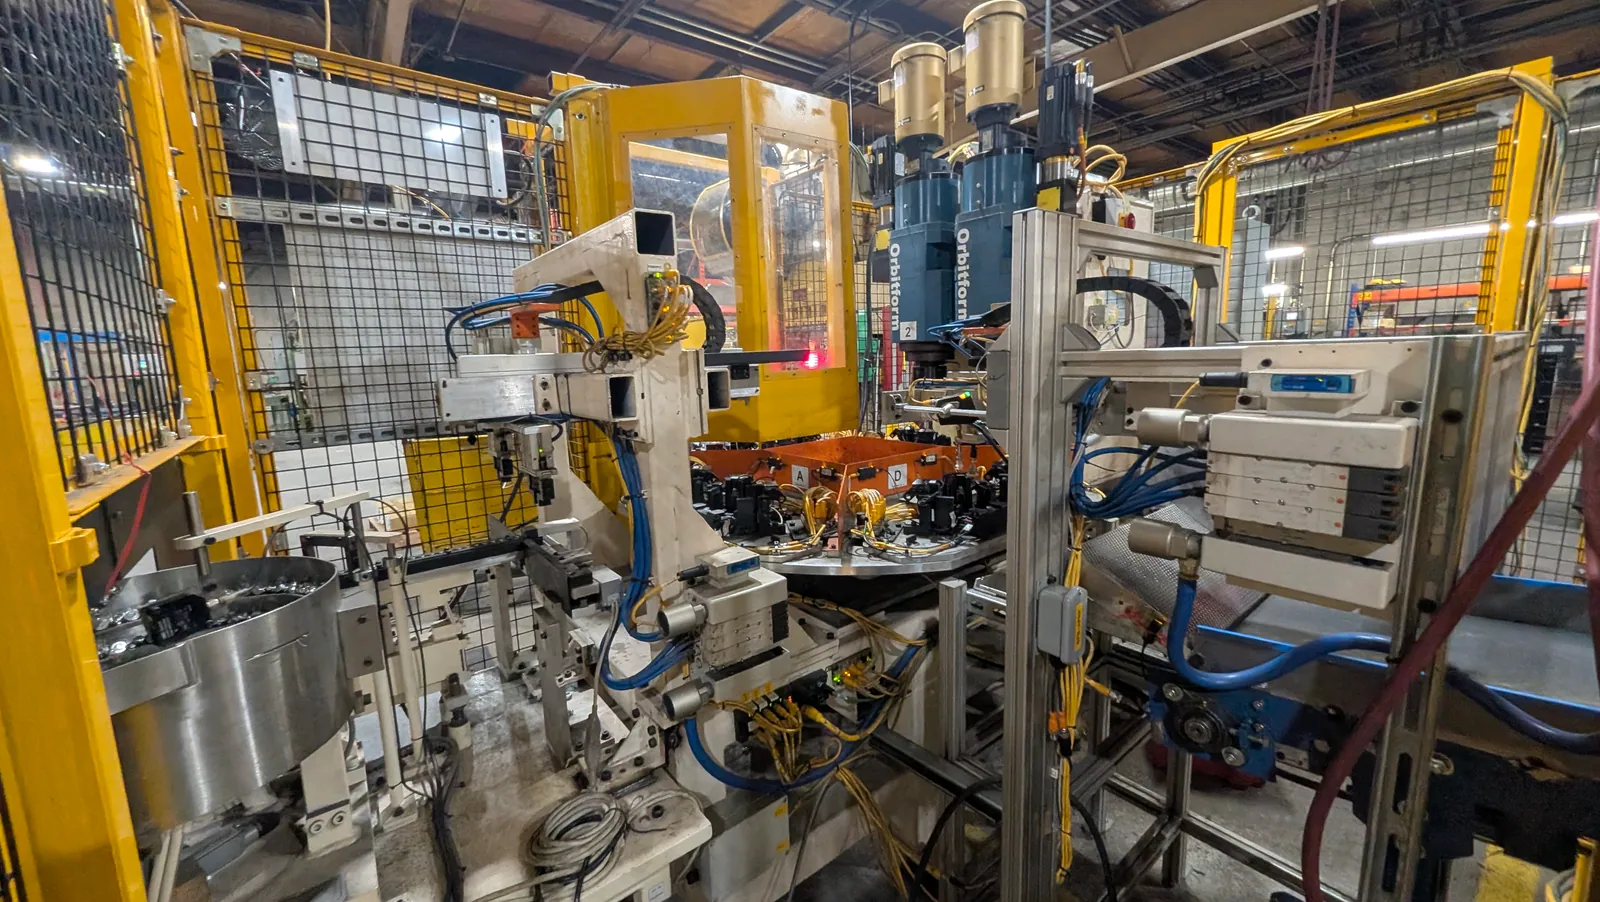
Mechanical automation and manual lines for finished sub-assemblies and modules.
Multi-station assembly lines combining mechanical automation with skilled manual work. Staking, clinching, tapping, grinding and final pack — often integrated directly with the upstream stamping or welding cell for one-piece flow. Kits and sequenced shipments for module integrators and OEMs.
Tool & Die Build
Full in-house tool and die shop — Clover started here in 1979 and never stopped.
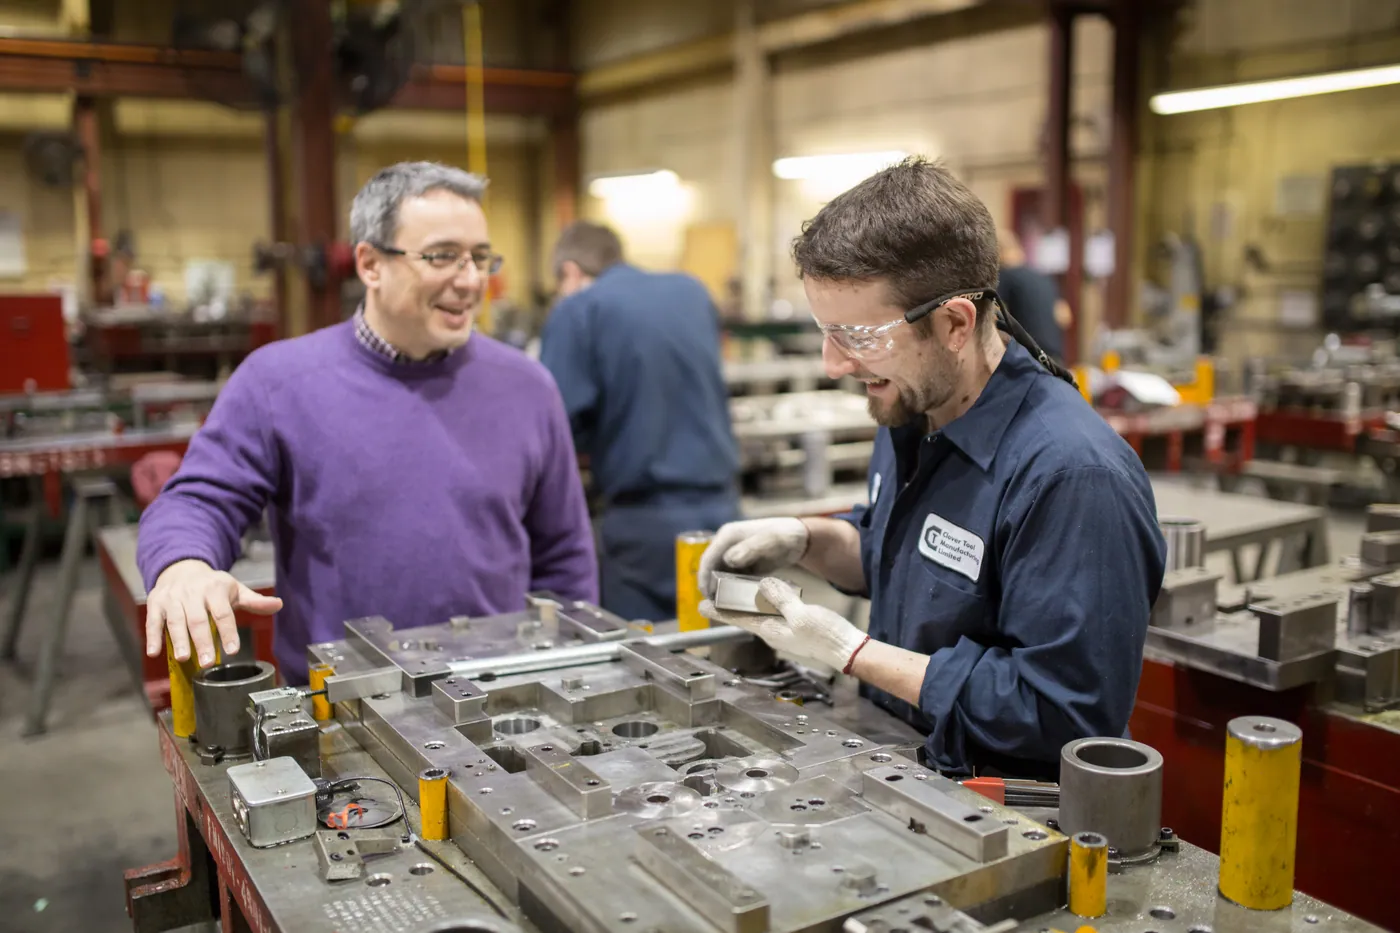
Clover Tool was founded as a tool and die shop and remains a full-service tool builder today. We design and build progressive dies, mechanical-transfer dies, hand-transfer dies, prototype tooling and weld fixtures in-house, with AutoForm forming simulation before any steel is cut. We build for our own presses and, when timing helps a program, for customer production lines. Rapid try-out on the same press the production tool will run on. Calibrated CMM and scanning-arm inspection on every die. The tool room handles repair, retro-fit and engineering changes for tools that have been in service for decades.
Value-Added Services
APQP engineering, prototyping, dimensional inspection and managed outsourced operations.
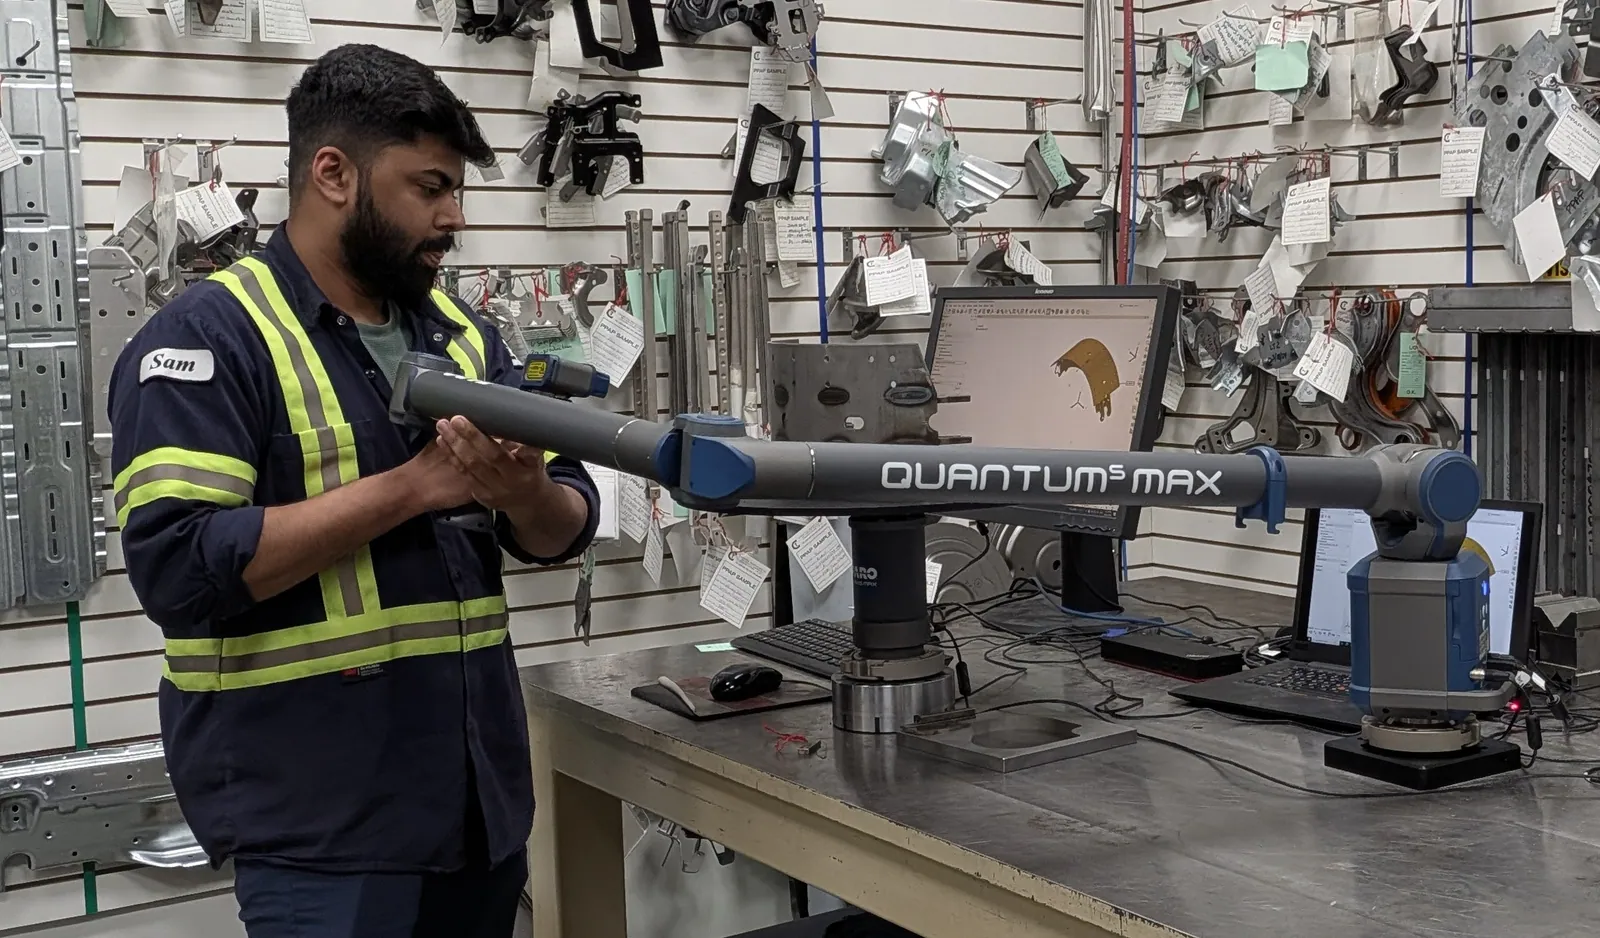
Every Clover program runs on the APQP five-phase process from internal kick-off to customer-approved PPAP. DFM/DFA review on every quote. First-article and in-process CMM inspection on every die. Gage management, calibration and SPC backing every line. Outsourced processes (etching, e-coating, washing) managed to spec and traced alongside internal steps. Coil-to-shipment traceability across every facility.
Processes
- APQP 5-phase program management
- DFM / DFA engineering review
- In-house prototyping
- First-article and in-process CMM inspection
- Gage management, calibration and SPC
- Coil-to-shipment traceability
- Managed outsourced operations (etching, e-coating, washing)
Equipment
- Portable CMM scanning arm
- CMM inspection
- Digital work instructions on tablets
Engineering & APQP
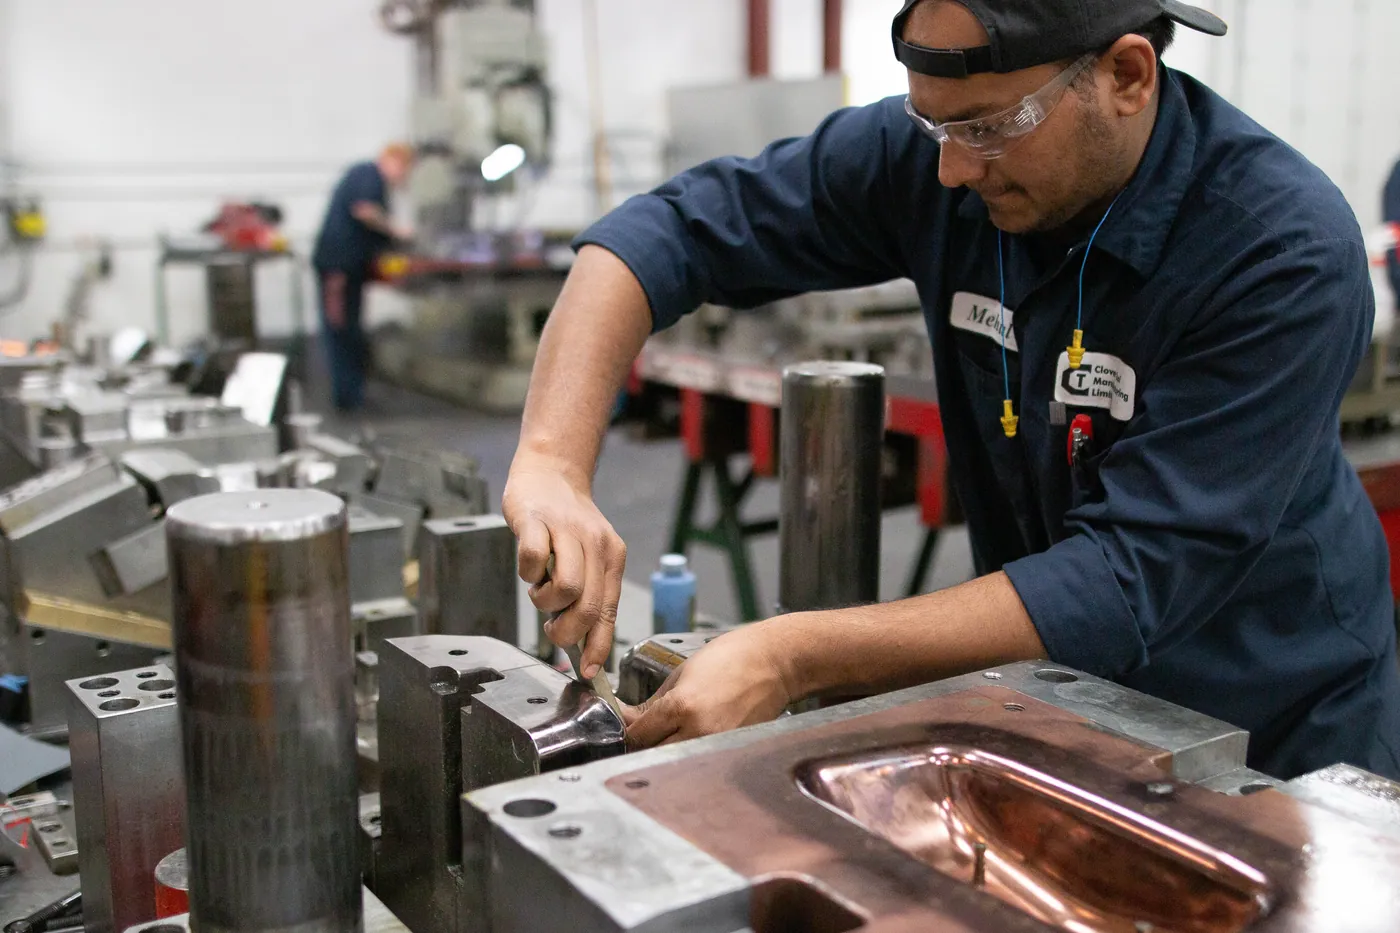
DFM/DFA review from RFQ. Five-phase APQP program management. PPAP to customer-approved launch.
Inspection & Traceability
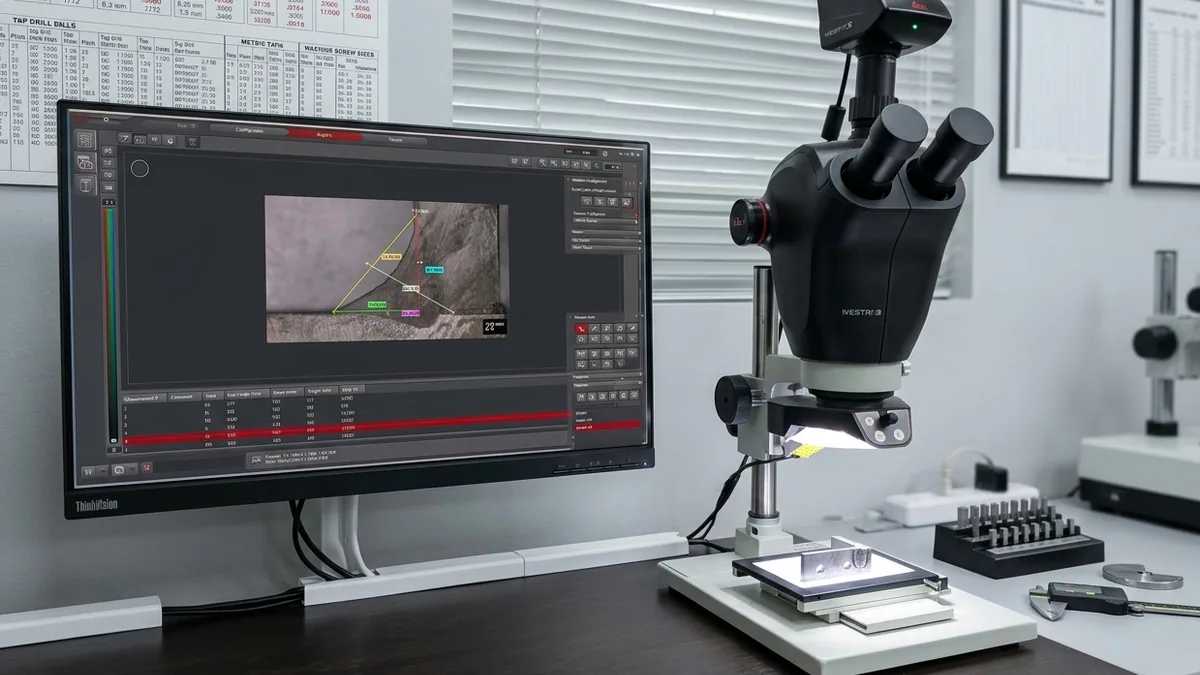
Scanning-arm, CMM and optical measurement, SPC data collection, coil-to-shipment traceability.
Every major product group on a modern vehicle.
From Body-in-white structures to powertrain components and seat tracks, Clover programs span the product groups integrators and OEMs rely on us for.
Body
Body-in-white structures, hinges, closures hardware.
- Hood hinges
- Trunk hinges
- Fender mounts
- Reinforcement components
Chassis & Brake Systems
Control arms, brake hardware (disc and drum), reinforcements and mounting structures.
- Control arms
- Disc brake brackets & hardware
- Drum brake hardware
- Support brackets
Powertrain
Heat exchangers, flex & drive plates, pedal assemblies.
- Heat exchanger components
- Transmission flex plates
- Transmission drive plates
- Pedal assembly components
Seating
Recliner components, seat tracks and adjuster sub-assemblies.
- Recliner components
- Seat tracks
- Seat track components
- Seat adjuster components
Closures & Window Systems
Door hardware, hand-brake assemblies, window regulator components.
- Door hinges
- Door locks
- Hand-brake assemblies
- Window regulator components
Five phases. One program, end-to-end.
Every Clover program runs the IATF 16949 APQP five-phase workflow. We manage it from the customer RFQ through Start of Production and program handoff. Honest milestones, real cost breakdowns, and a senior engineer owning the line.
- Phase 1
Planning
Internal program kick-off. Concept review, DFM / DFA, cost model, timing plan.
- Phase 2
Process design kick-off
Tool, fixture and equipment design. Process FMEA. Buy-off on process concept with customer.
- Phase 3
Tool & fixture build
In-house tool build. Rapid try-out. Gage design and build. Customer-witnessed tool delivery.
- Phase 4
Home-line tool + PPAP
First-article runs on production line. Capability studies. Customer-approved PPAP submission.
- Phase 5
Manufacturing buy-off + SOP
Full-rate validation, manufacturing buy-off, Start of Production, program handoff.
Registered at the audit level.
Both facilities are IATF 16949:2016 and ISO 9001:2015 registered; Concord additionally holds ISO 14001:2015. Customer Specific Requirements (CSR) maintained in the CSR matrix. Full capability sheet and quality manual available on request.
Asked on most first calls.
The questions buyers usually open with. Capability-specific questions live on the metal stamping , tool & die and robotic welding pages. Anything else, ask us directly.
What does Clover Group do in-house?
Metal stamping from 80 to 1,650 tons, tool and die design and build with AutoForm forming simulation, robotic welding, sub-assembly and value-added services such as APQP engineering and CMM inspection, at two Ontario plants in Concord (Toronto / GTA) and Breslau (Waterloo Region). Metal stamping, tool and die, and robotic welding each have their own page with full equipment lists.
Do you design parts, or build to print?
We build to print: product design stays with the customer and is outside our IATF 16949 scope. We design everything it takes to make the part, including progressive and transfer dies, weld fixtures and the forming process itself, using AutoForm simulation. Every quote comes with DFM/DFA feedback.
Can you take over a program from a distressed supplier?
Yes. Clover takes over programs from distressed or exiting suppliers. The in-house tool room repairs, retro-fits or rebuilds the transferred dies, try-out runs on our own presses, and the program re-launches through our APQP and PPAP workflow under IATF 16949, with the aim of getting parts shipping again as quickly as possible.
Do you offer e-coating or other finishing?
Yes, as managed outsourced processes. E-coating, etching and washing are run by outside suppliers, managed to spec and traced alongside our internal steps, so parts ship finished with one record from coil to shipment.
Let’s build what’s next — together.
Drop us your drawings, volumes, and timing. A senior engineer will be back within one business day with a real conversation, not a templated auto-reply.